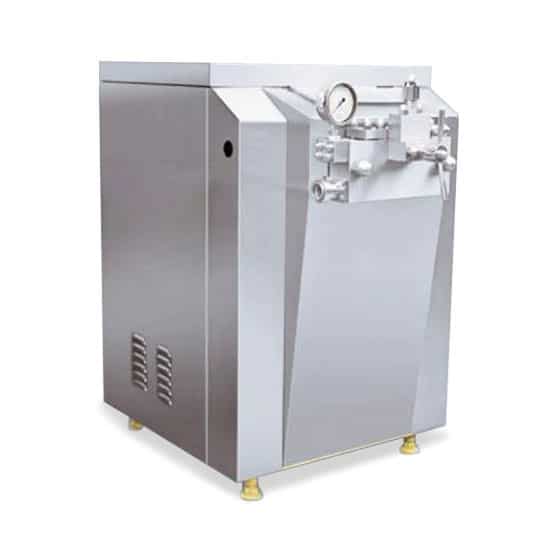
The dairy homogenization machine is a critical piece of equipment in modern dairy processing, designed to transform the physical properties of milk through high-pressure processing. This milk homogenizer reduces fat globule size from the natural 3-5 microns to less than 1 micron, creating a stable, uniform mixture where fat particles remain suspended rather than rising to the surface. The result is dairy products with smoother texture, better mouthfeel, improved nutritional absorption, and significantly extended shelf life. Whether you’re operating a small yogurt shop or a large-scale dairy processing facility, understanding the role of homogenization in dairy production is essential for achieving consistent, high-quality products that meet consumer expectations.
High-Pressure Technology: 15-25 MPa | SUS 304 Construction | Two-Stage Homogenization | 200-5000L/hr Capacity
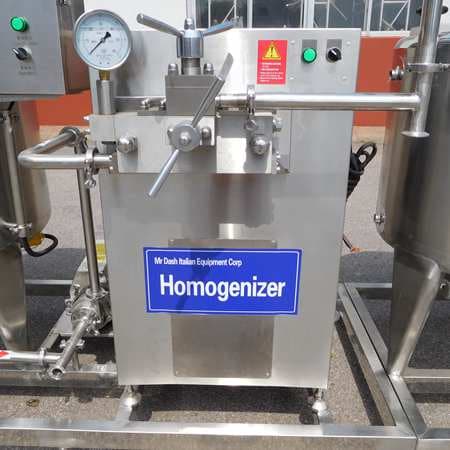
Why Homogenization is Essential in Dairy Processing
In untreated milk, fat globules are relatively large and have a tendency to rise to the surface due to density differences - this is the cream layer you may have observed in untreated milk. This natural separation presents several challenges for dairy processors: inconsistent product texture, unappealing appearance, and reduced shelf stability. The milk homogenizer solves these problems by mechanically reducing fat globule size and creating an emulsion where fat remains evenly distributed throughout the product.
The Science of Fat Globule Size Reduction
Unhomogenized milk fat globules typically range from 1-15 microns in diameter, with an average around 3-5 microns. These larger globules rise to the surface due to buoyancy (Stokes’ Law), forming a visible cream layer within 24-48 hours.
Homogenization reduces this size to less than 1 micron through high-pressure mechanical processing. At this size, the fat globules remain permanently suspended and do not separate, creating a stable emulsion that can last for weeks or months.
Impact on Yogurt Production
For yogurt production, homogenization is particularly important because it directly impacts the final texture, appearance, and quality of the yogurt:
| Homogenization Effect | Without Homogenization | With Homogenization |
|---|---|---|
| Fat Distribution | Uneven, rises to surface | Uniformly distributed |
| Texture | Grainy, inconsistent | Smooth, creamy |
| Whey Separation | Visible after 24 hours | Minimal or none |
| Shelf Life | 7-14 days | 14-21 days |
| Fermentation Consistency | Variable batch quality | Consistent results |
Understanding Homogenization Technology
Single-Stage vs. Two-Stage Homogenization
The homogenization process can be configured as single-stage or two-stage, each with distinct advantages:
| Configuration | First Stage | Second Stage | Best For |
|---|---|---|---|
| Single-Stage | 15-25 MPa | None | Standard yogurt, fresh milk |
| Two-Stage | 20-25 MPa | 3-5 MPa | Greek yogurt, high-fat products, premium dairy |
Two-stage homogenization is essential for high-fat dairy products because:
- Prevents Re-coalescence: After the first stage breaks down fat globules, the second stage at lower pressure prevents them from recombining
- Improves Emulsion Stability: Creates more stable bonds between fat globules and proteins
- Better Texture Development: Critical for thick, creamy Greek yogurt and premium products
Why Pressure Matters: Technical Deep-Dive
The relationship between homogenization pressure and fat globule size follows predictable patterns:
| Pressure | Average Globule Size | Resulting Texture | Best Application |
|---|---|---|---|
| 10 MPa | 1.5-2.0 microns | Light, pourable | Drinking yogurt |
| 15 MPa | 1.0-1.5 microns | Smooth, medium body | Standard yogurt |
| 20 MPa | 0.5-1.0 microns | Thick, creamy | Premium yogurt |
| 25 MPa | < 0.5 microns | Very thick, premium | Greek yogurt, labneh |
The Science: Cavitation and Shear Effects
The high-pressure homogenizer works through two main physical effects:
Cavitation Effect: When milk accelerates through the homogenizer gap at high pressure, static pressure drops below fat’s saturated vapor pressure, causing cavitation (microbubble formation). The collapse of these bubbles creates localized shock waves that mechanically crush fat globules. This effect is particularly effective for breaking down large fat aggregates.
Shear Effect: High-velocity flow through narrow homogenizing valve gaps generates powerful shear forces (fluid shear). These shear forces deform, elongate, and ultimately pulverize fat globules into fine particles. The combination of cavitation and shear effects ensures complete homogenization.
Types of Homogenization Equipment
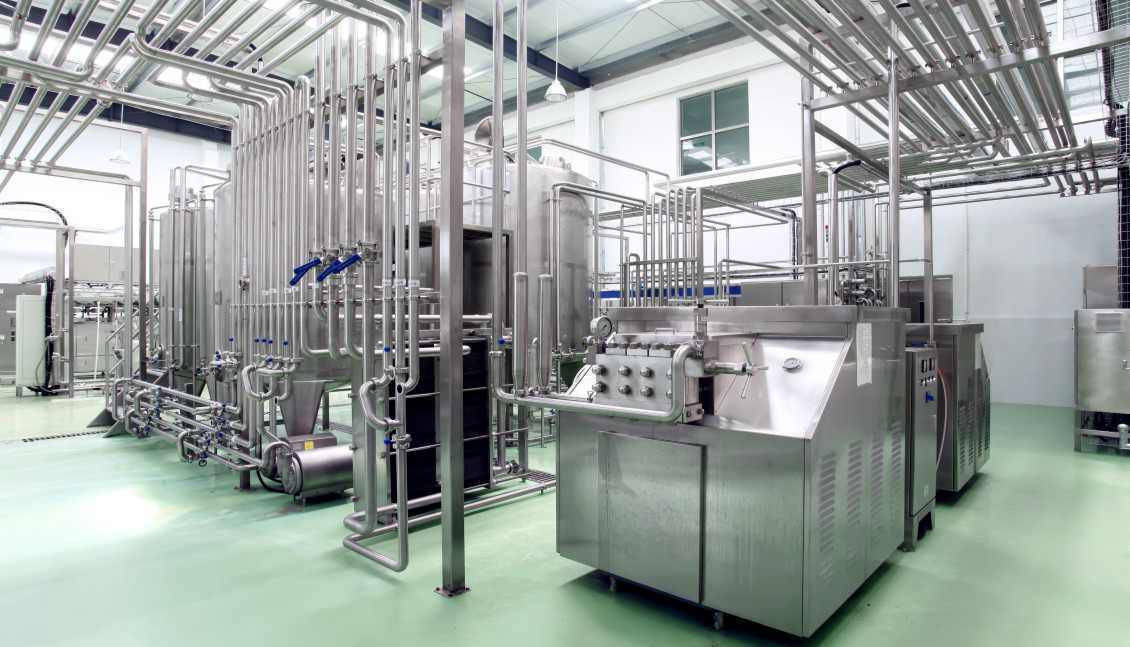
Modern dairy processing facilities utilize several types of homogenization equipment:
| Type | Pressure Range | Capacity | Best Application | Price Range |
|---|---|---|---|---|
| High-Pressure Homogenizer | 15-25 MPa | 200-5000L/hr | Commercial yogurt | $8,000-$50,000 |
| Two-Stage Homogenizer | 20-25 + 5 MPa | 500-10000L/hr | Premium dairy, Greek yogurt | $15,000-$80,000 |
| Ultrasonic Homogenizer | Acoustic | Up to 100L/hr | Laboratory, research | $5,000-$20,000 |
| Inline Homogenizer | 10-20 MPa | 1000-20000L/hr | Continuous production | $20,000-$100,000+ |
For most commercial yogurt production applications, the high-pressure homogenizer with two-stage configuration offers the best balance of efficiency, effectiveness, and cost.
Shuliy vs. Competitors: Technical Comparison
| Feature | Shuliy Homogenizer | Typical Competitor |
|---|---|---|
| Pressure Range | 15-25 MPa | 10-20 MPa |
| Two-Stage Design | Standard | Often single-stage |
| Plunger Material | Ceramic-coated | Standard steel |
| Valve Material | Tungsten carbide | Stainless steel |
| Temperature Control | Built-in heating | External required |
| Pressure Stability | +/- 0.5 MPa | +/- 1-2 MPa |
| Continuous Operation | 24/7 capability | 8-12 hours |
| Motor Efficiency | IE3 premium efficiency | IE2 standard |
| Noise Level | < 85 dB | 90-95 dB |
| Warranty | 2 years | 1 year |
Key Technical Advantages
Superior Valve Technology: Our homogenizing valves are manufactured from tungsten carbide, providing 3x longer service life compared to standard stainless steel valves. The precision-machined valve seats ensure consistent pressure distribution across the homogenizing gap.
Advanced Seal Design: Proprietary seal technology prevents pressure leakage and extends maintenance intervals by 40%.
Premium Motor Efficiency: IE3 premium efficiency motors reduce energy consumption by 10-15% compared to standard motors, significantly lowering operating costs.
Role in Yogurt Production
In the yogurt production line, the homogenizer requires milk preheating to approximately 55C for optimal fat globule membrane elasticity. A milk preheating machine is positioned before the homogenizer to ensure proper temperature before processing. After homogenization, the milk proceeds to sterilization, creating the optimal foundation for yogurt fermentation.
Optimal Processing Parameters
| Parameter | Recommended Value | Effect of Deviation |
|---|---|---|
| Preheating Temperature | 50-60C | Below 45C: poor homogenization |
| Homogenization Temperature | 55-70C | Above 70C: protein denaturation |
| First Stage Pressure | 20-25 MPa | Lower: incomplete homogenization |
| Second Stage Pressure | 3-5 MPa | Absent: re-coalescence risk |
| Fat-to-Casein Ratio | 0.2g casein/g fat | Affects texture stability |
Homogenization quality depends on several interconnected factors: temperature, pressure, and the fat-to-casein ratio (ideally 0.2g casein per gram of fat). When these parameters are optimized, the result is milk that ferments evenly, produces yogurt with superior texture, and maintains quality throughout its shelf life.
Structure & Components
The milk homogenizing machine is a three-plunger reciprocating pump consisting of precision-engineered components:
Core Components
| Component | Function | Maintenance Interval |
|---|---|---|
| Main drive shaft | Converts motor rotation to reciprocating motion | 12 months |
| Transmission belt | Transfers power to pump assembly | 6 months |
| Plungers (3x) | Generates high-pressure flow | 3-6 months |
| Suction valves | Controls milk entry to cylinder | 6-12 months |
| Discharge valves | Controls milk exit under pressure | 6-12 months |
| Homogenizing valve | Primary homogenization site | 3-6 months |
| Pressure gauge | Monitors operating pressure | 12 months |
| seals and gaskets | Maintains pressure integrity | 3-6 months |
Three-Plunger Design Advantages
The three-plunger configuration provides several advantages over single or dual-plunger designs:
- Continuous Flow: One plunger is always in the discharge stroke, ensuring uninterrupted production
- Reduced Pulsation: Three overlapping pressure cycles minimize pressure fluctuations
- Balanced Operation: Equal load distribution across three plungers reduces wear
- Higher Efficiency: More complete milk processing with each stroke cycle
Operating Guidelines for Optimal Results
Temperature Management
Always preheat milk to 50-60C before homogenization. At this temperature range, fat globule membranes are most elastic and can be broken down most effectively.
- Below 45C: Fat is too solid for proper emulsification
- Above 65C: Protein denaturation may occur
- Optimal range: 55-70C for most yogurt applications
Pressure Optimization
For standard yogurt production, operate at 15-20 MPa in the first stage and 3-5 MPa in the second stage. Higher pressures (up to 25 MPa) may be used for high-fat products or when producing premium-grade yogurt with extra smooth texture.
Flow Rate Control
Maintain consistent flow rates through the homogenizer. Sudden pressure changes can damage valves and reduce homogenization efficiency. Use variable frequency drives to adjust flow rates for different batch sizes.
Pre-Filtration Requirement
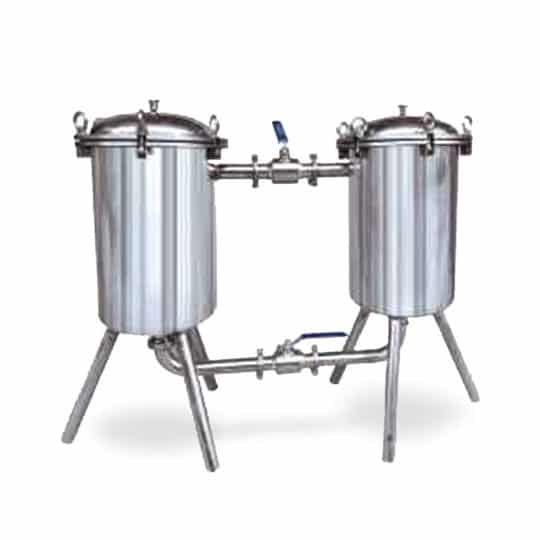
Always filter raw milk before homogenization to remove debris, hair, and other particles that could clog the homogenizing valve or damage plungers. Install a 100-200 mesh filter upstream of the homogenizer.
Quality Verification Methods
Visual Inspection
Signs of proper homogenization include:
- No visible cream layer after 24 hours of storage
- Uniform white appearance without yellowish tint
- Smooth, consistent texture
Microscopic Analysis
Regular testing with a microscope to observe fat globule size is the most reliable indicator:
- Proper homogenization: < 1 micron average
- Under-homogenized: 1-3 microns with visible variation
- Poor homogenization: > 3 microns with cream separation
Stability Testing
Perform shelf stability tests:
- 24-hour test: No visible separation
- 7-day test: Minimal whey separation acceptable
- 14-day test: Should maintain smooth texture
Economic Analysis: ROI of Homogenization
Cost Comparison
| Factor | Without Homogenizer | With Homogenizer | Savings |
|---|---|---|---|
| Product Value | Base price | Premium pricing (+15-20%) | $0.15-0.20/cup |
| Shelf Life | 7-14 days | 14-21 days | 50% extension |
| Wastage | 3-5% | < 1% | 2-4% of production |
| Customer Complaints | Frequent | Rare | Immeasurable |
Payback Calculation
For a 1000L/day yogurt operation:
- Equipment investment: $20,000-35,000
- Annual production: 300,000 liters
- Value increase from premium product: $45,000/year
- Reduced wastage savings: $6,000/year
- Energy cost addition: $2,000/year
- Net annual benefit: $49,000
- Payback period: 5-7 months
Maintenance Schedule
Daily Operations
Check oil levels, listen for unusual noises, and verify pressure gauge readings before each production run.
Weekly Maintenance
Inspect seals and gaskets for wear, clean homogenizing valves, and check belt tension.
Monthly Service
Replace worn seals, inspect suction and discharge valves, and calibrate pressure sensors.
Annual Overhaul
Complete inspection of plungers, valve seats, and bearings; replace all wear parts; verify mechanical integrity.
Technical Specifications
| Parameter | Specification |
|---|---|
| Equipment Type | High-pressure homogenizer |
| Main Structure | Three-plunger reciprocating pump |
| Material | SUS 304 stainless steel |
| Optimal Temperature | 55-70C |
| Operating Pressure | 15-25 MPa |
| First Stage | 15-25 MPa adjustable |
| Second Stage | 3-5 MPa adjustable |
| Capacity | 200-5000L/hr |
| Motor Power | 7.5-45 kW depending on model |
| Applications | Dairy, beverages, biotechnology, pharmaceuticals |
Frequently Asked Questions
Q: What is the difference between single-stage and two-stage homogenization?
A: Single-stage homogenization uses one homogenizing valve at high pressure. Two-stage homogenization adds a second valve at lower pressure (typically 3-5 MPa) after the first stage. The second stage prevents fat globule re-coalescence and is especially important for high-fat dairy products like cream or yogurt, ensuring long-term stability and consistent texture.
Q: Can homogenization replace pasteurization?
A: No, homogenization and pasteurization serve different purposes. Homogenization is a mechanical process that reduces fat globule size, while pasteurization is a heat treatment that destroys pathogenic bacteria. Both processes are typically used in yogurt production for different purposes.
Q: How do I know if my homogenizer is working properly?
A: Signs of proper homogenization include: no visible cream layer after 24 hours of storage, smooth texture in finished yogurt, and consistent results batch to batch. Regular testing with a microscope to observe fat globule size (should be less than 1 micron) is the most reliable indicator of homogenization efficiency.
Q: What maintenance is required for the homogenizer?
A: Daily inspection includes checking oil levels and pressure readings. Weekly maintenance includes inspecting seals and cleaning valves. Monthly service includes replacing worn seals and calibrating sensors. Annual overhaul includes complete inspection of plungers and bearings.
Related Products
For complete dairy processing solutions, explore our complementary equipment:
- Yogurt Production Line - Complete turnkey solution integrating homogenization as a key processing stage
- Milk Pasteurizer Machine - Sterilizes homogenized milk for safe consumption
- Yogurt Duplex Filter - Pre-filtration equipment for raw milk before homogenization
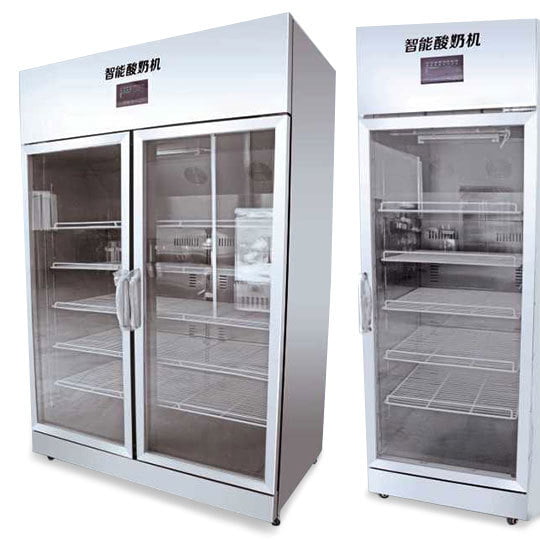
- Yogurt Fermentation Maker - Ferments sterilized and homogenized milk into yogurt